Express Offer. Receive your RFQ within 12 hours.
Manufacturing metallurgy & tribology

Engineered at the molecular & micron level.

Every DUO-CONE mechanical face seal is the outcome of specialised metallurgy, proprietary centrifugal casting, precision lapping and rigorous elastomer formulation, designed to resist abrasive slurry, extreme load and high sliding velocities.

DUO-CONE precision-engineered mechanical face seals Live optical sensor feed · 4K metrology01Lapped mirror face< 0.13 µm Ra flatness02Ni-Hard alloy matrix60 – 70 HRC martensitic03Toric elastomerISO 3601 calibrated
Tolerance0.000 mm
Hardness0 HRC
Velocity0 m/s
[ Cross-section engineering ]

Interactive seal anatomy

Pick a component to see how complementary mechanical forces guarantee zero leakage under high particulate intrusion.

Spec: Ni-Hard 4 / 15-3 chromium

High-wear resistant alloy matrix

Engineered to withstand direct contact against hyper-abrasive quartz, crushed granite and coal slurry. The hardened carbide network holds hardness under sustained friction temperatures above 200 °C.

Hardness scale60 – 72 HRC
Service life> 12,000 op. hours
[ Process architecture ]

The 6 core technologies

From molten-alloy centrifugal pouring to optical helium testing, every phase reflects rigorous German manufacturing standards.

Centrifugal castingPhase [01/06]1600 °C induction

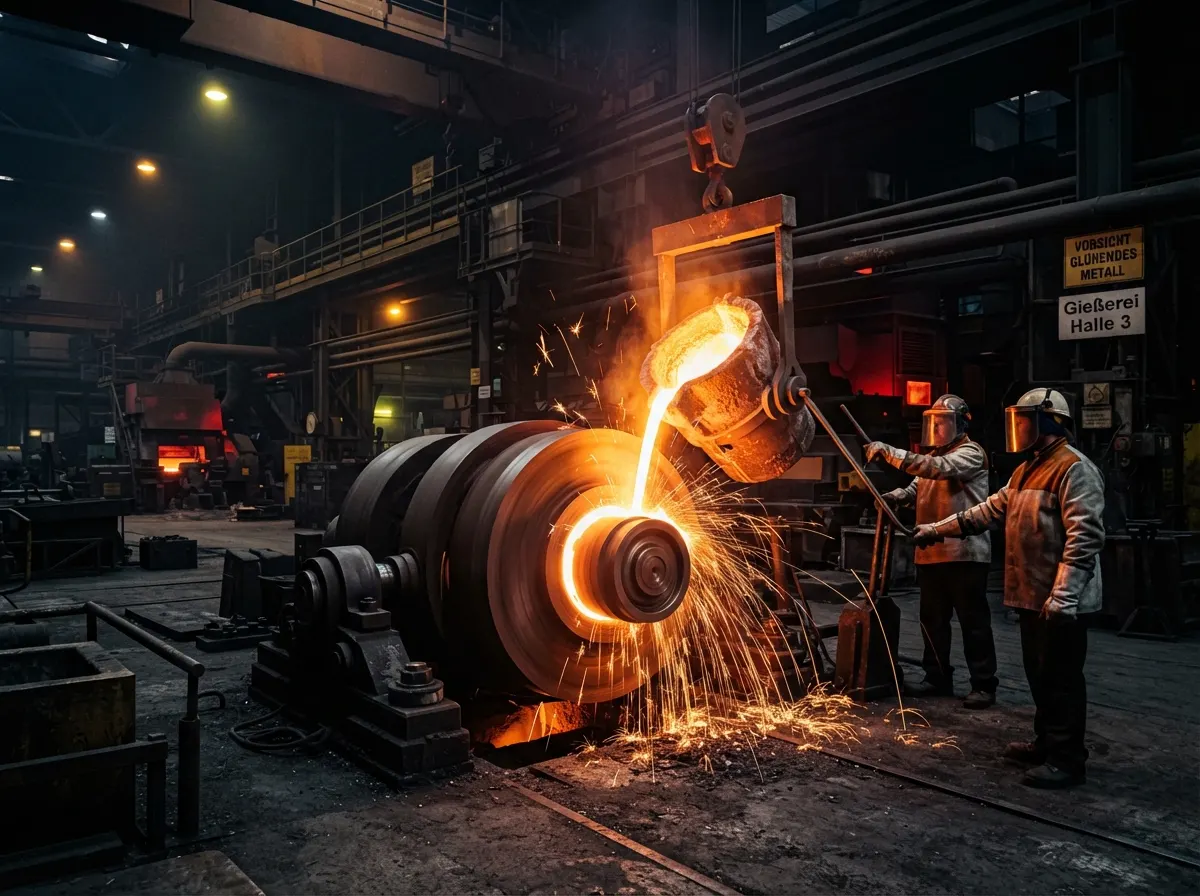
01 Centrifugal casting

Molten Ni-Hard cast iron is spun into cylindrical dies at thousands of RPM. Centrifugal force drives out air pockets and voids, pushing impurities to the bore for an ultra-dense, homogeneous carbide microstructure.

Void-free densityContinuous grain alignment
Precision CNC & optical lappingPhase [02/06]2 helium light bands

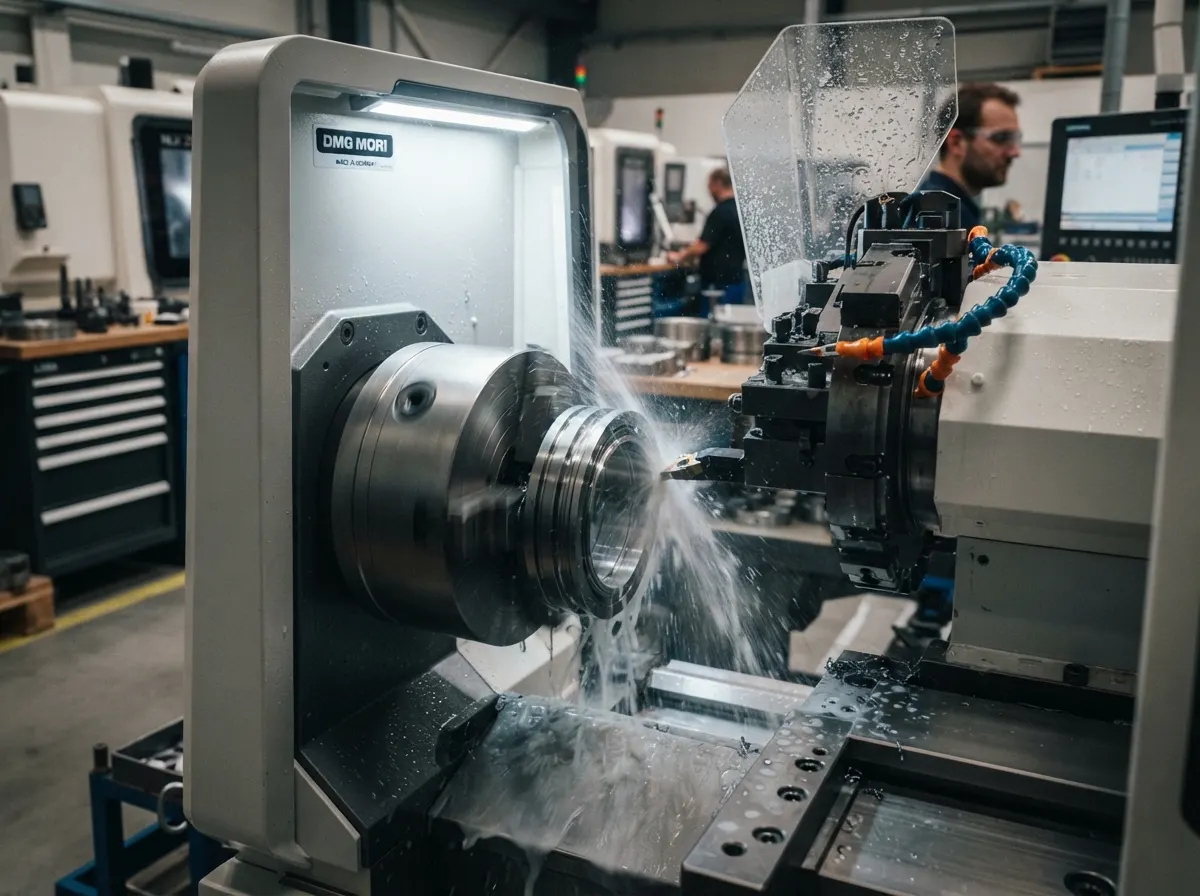
02 Precision CNC & optical lapping

Robotic CNC lathes profile the sealing contours to micrometre repeatability. Three-stage orbital lapping with diamond slurry then yields a mirror finish, verified by monochromatic light-band interferometry.

Ra < 0.13 µmHydrodynamic boundary wedge
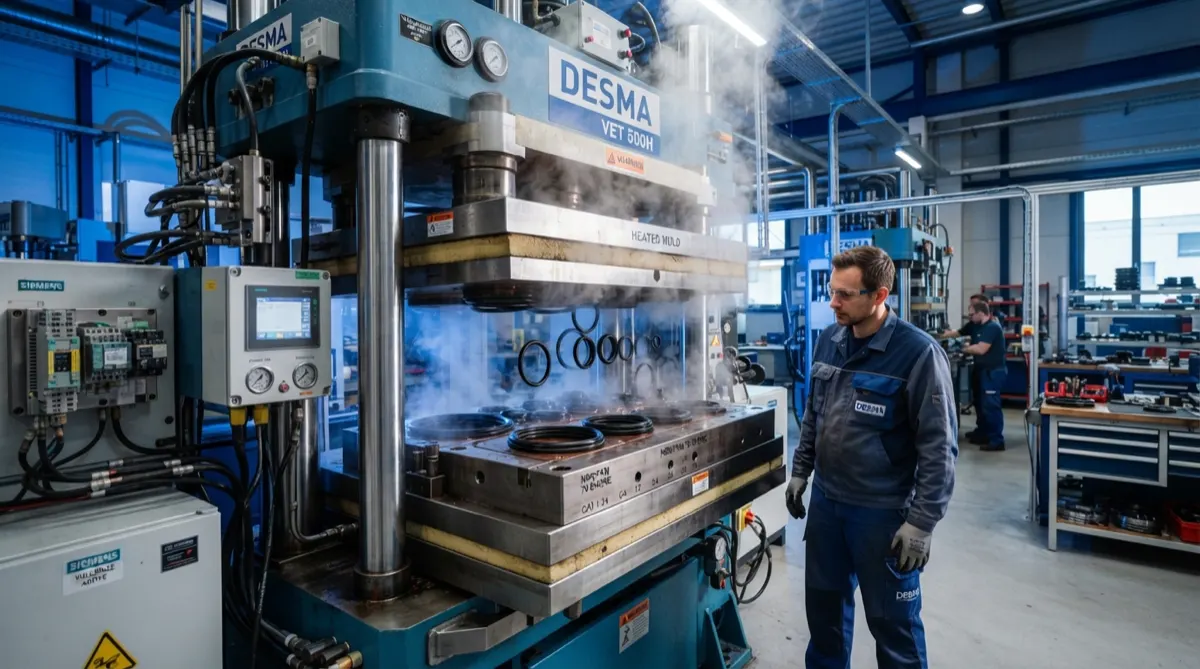
Compression rubber mouldingPhase [03/06]Vulcanisation press · NBR & FKM

03 Compression rubber moulding

Toric rings are formulated and moulded under strict temperature cycles for uniform elasticity, minimal compression set and long-term axial spring load across thermal swings.

NBR −40 → +100 °CHNBR ozone-resistantFKM −20 → +200 °CSilicone −60 °C
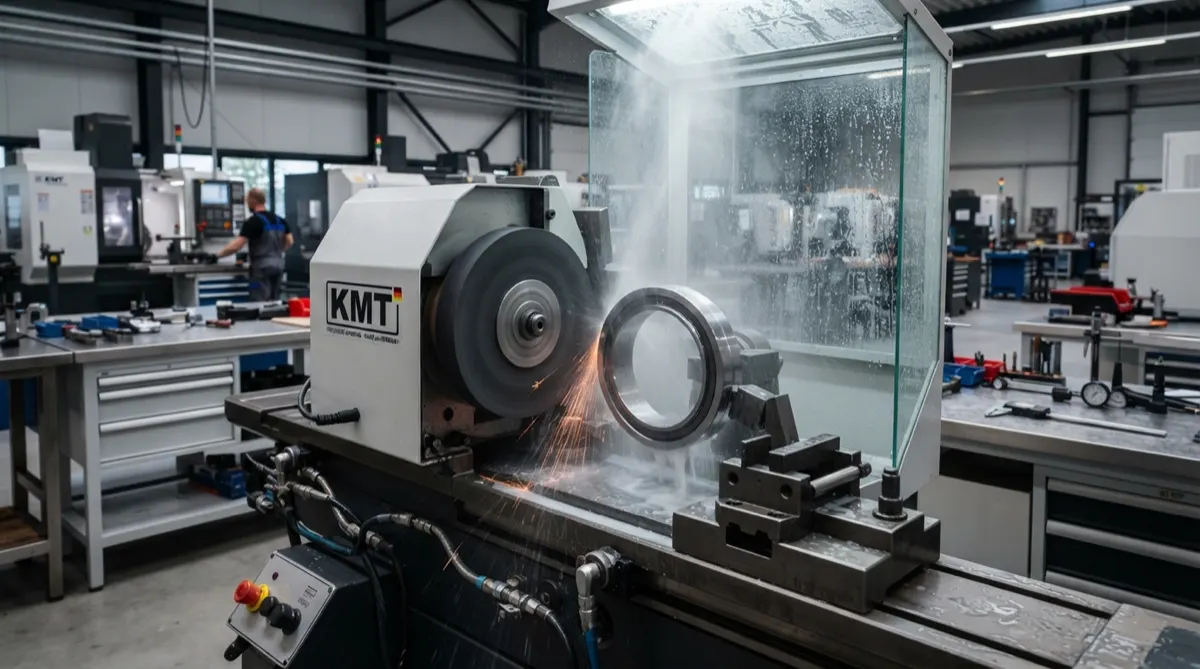
Precision grindingPhase [04/06]Centerless grinding · ±0.005 mm

04 Precision grinding

Centerless external, bore and face grinding hold tight diametrical concentricity. This kills wobble and prevents localised toric pinching under shock loading.

Diametrical concentricity ±0.005 mm
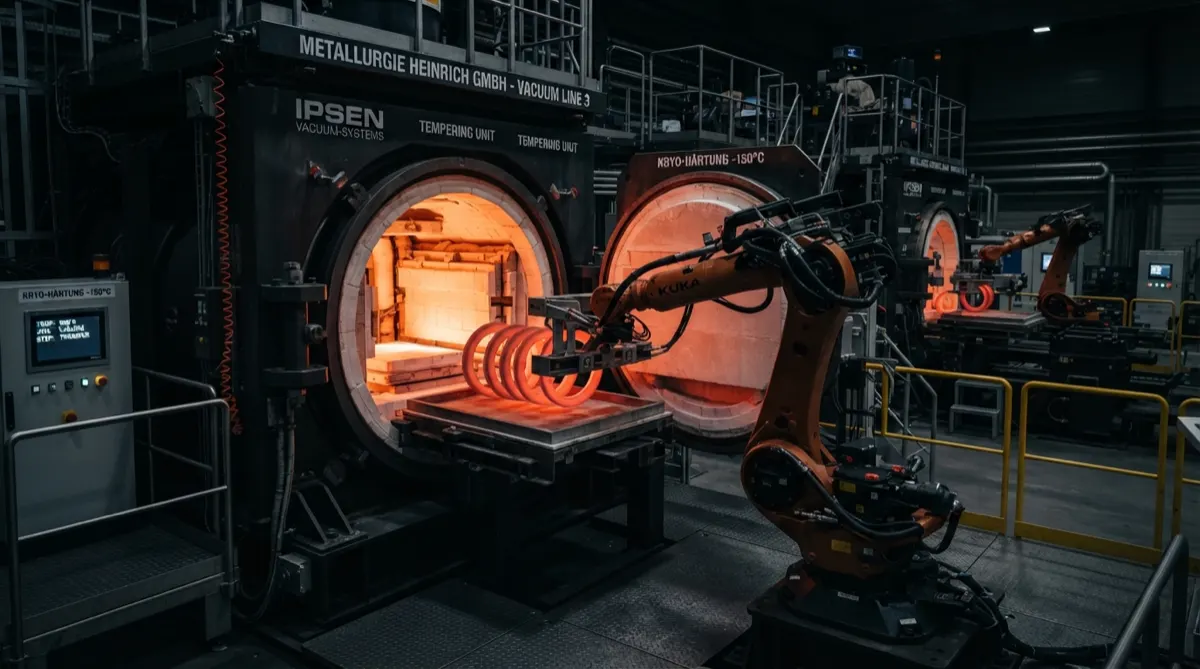
Heat treatmentPhase [05/06]Vacuum furnace · cryogenic

05 Heat treatment

Tailored metallurgical transformation delivers the exact balance of core shatter toughness and contact-face abrasion resistance.

Sub-zero cryogenicInduction hardeningTemperingGas nitridingLaser hardening
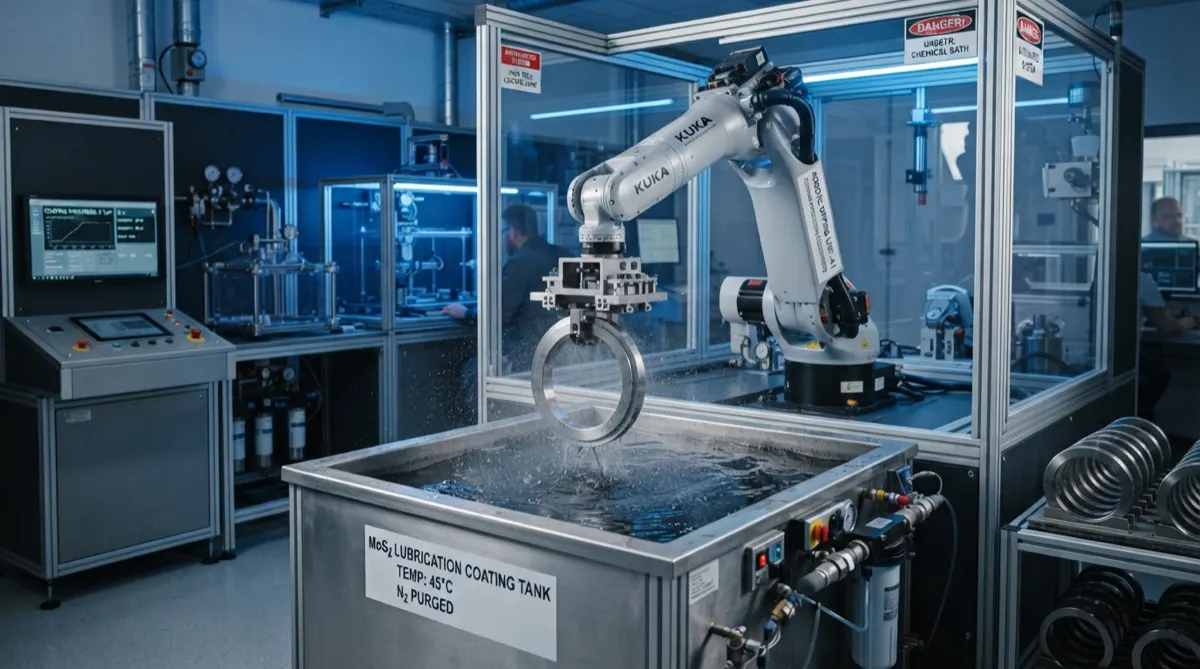
Surface treatments & coatingsPhase [06/06]Tribological coating · MoS₂ & WS₂

06 Surface treatments & coatings

Electrochemical and dry-film tribological treatments guard against corrosion, fretting wear and dry-startup galling.

MoS₂ dry lubricantWS₂ 0.03 µ frictionCED electro-coatingZn passivation > 500 h salt spray
Pending patents / ongoing development

DUO-CONE research lab

Continuously testing metallurgy under extreme simulation inside our Engelskirchen facilities.

R&D Module 01v ≤ 10 m/s
High-speed sliding surface velocity

Balanced micro-groove profiles that channel cooling oil into hydrodynamic film barriers during high-RPM continuous transit.

R&D Module 02FEA tribo-model
Wear-life tribology modelling

Lifecycle algorithms simulating quartz sand, taconite and mud ingress to predict seal-envelope failure before it happens in the field.

R&D Module 03Viscoelasticity
Elastomeric stress relaxation

Polymer chains formulated to resist permanent compression set across sub-zero arctic and ultra-high desert thermal swings.

R&D Module 04Nano-barrier
Slurry protection coatings

Plasma-sprayed nanoceramic shields across the seal ramp zone to repel dense iron-ore tailings and abrasive gravel buildup.

R&D Module 05Carbide matrix
Ni-Hard alloy optimisation

Refinement of molybdenum and nickel ratios to eradicate micro-chipping while amplifying fracture toughness on heavy track drives.

[ Validation ]

Seal life testing

Which tests we run on every duo cone face seal before it leaves Engelskirchen.

T1
Stage 1 / 5Contamination

Mud packing test

  • Mud-submerged wear and leakage under a contamination load
T2
Stage 2 / 5Thermal

Heat generation test

  • Time, pressure and surface speed in lubrication, measuring the heat the face pair generates
T3
Stage 3 / 5Rubber science

Elastomeric test

  • Oil compatibility
  • Face-load variation against time and temperature
  • O-ring squeezing
  • O-ring contraction
T4
Stage 4 / 5Tribology

P-V test

  • Pressure against velocity at linear speed
  • Wear, galling and spilling
T5
Stage 5 / 5Lifecycle rig

Seal endurance testing

  • Endurance rig running at set speed and temperature
  • Up to 1000 rpm to reach 10 m/s linear speed
  • Up to 1000 kgf axial load
  • Seal sizes 45 to 1200 mm outer diameter
[ FEA · contact model ]Contact-pressure simulationFinite-element map of face load and hydrodynamic film across the sealing band.
[ Direct engineering desk ]

Specific dimensional or metallurgical requirements?

Our senior seal engineers help with custom mould prototyping, CAD cross-referencing, material pairings and express OEM batch production.

Standard dispatch: 24 hoursDIN EN ISO 9001:2015100% optical test
Let’s work together

Get in touch to start your next project.

Questions, a part number to cross-reference, or a bulk requirement? Our German-based engineering team gives expert guidance and tailored seal solutions, and replies within one business day.

Headquarters & home of engineering